Industrial Revolution · 1800
Was the factory a revolution in machines or in control?
The seminar question: “Was the factory system more a revolution in machines or a revolution in the control of work?”
Between the 1760s and the 1780s Hargreaves’ spinning jenny, Arkwright’s water frame and Crompton’s mule mechanised cotton spinning. In 1771 Arkwright installed his machines in a mill at Cromford in Derbyshire and ran it in shifts, creating the factory, where workers tended powered machines under a manager’s rules.
WW2 is free — every chapter. Try chapters 1–2 of any 2 other atlases (3 with a free account). Opening a new atlas uses one of them. Membership opens all 21 — Join.
Free printable Industrial Revolution study guide, sent by email ↓
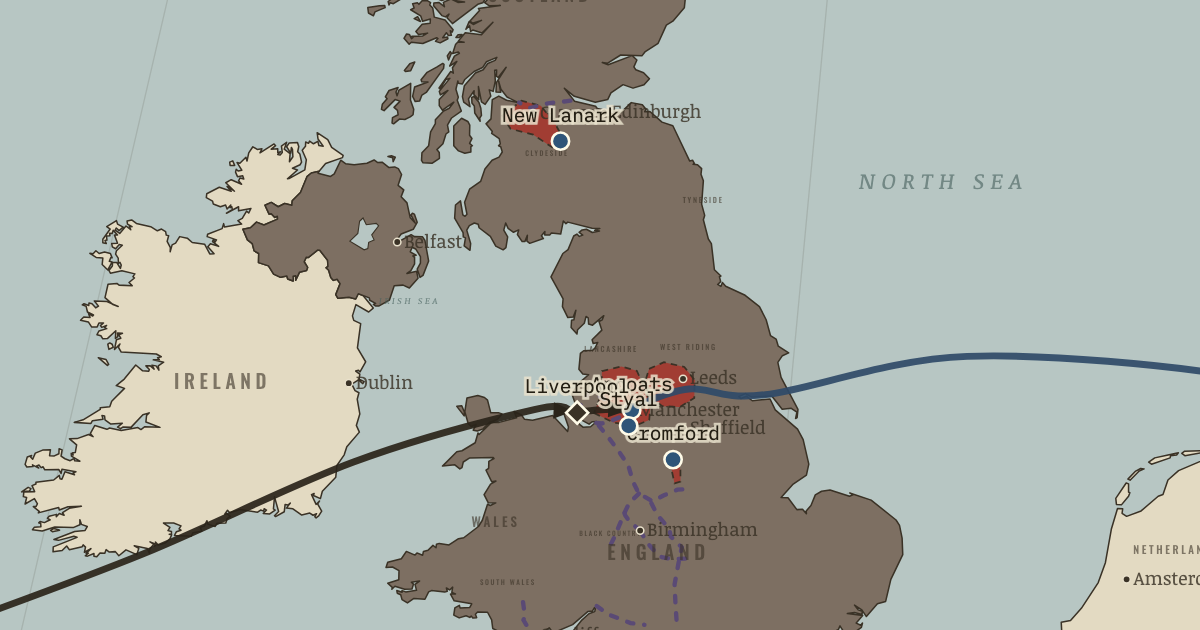
Cotton led the way because British producers had a clear model to copy and a protected market in which to copy it. Indian calicoes, light printed cotton cloths, had flooded English shops in the late seventeenth century, and Parliament banned imports of printed calicoes in 1700 and their wearing in 1721. Those Calico Acts left a home market hungry for cheap cotton cloth that British hand spinners could not supply, since their thread was too weak and too slow to make. Inventors therefore attacked that bottleneck, because whoever could spin cheap, strong thread would own the market. The weaver James Hargreaves’ jenny of about 1764 let one person spin many threads at once, the former wigmaker Richard Arkwright’s water frame, patented in 1769, spun thread strong enough for the lengthwise warp, and the spinner Samuel Crompton’s mule of 1779 spun it fine. The economic historian Robert Allen’s figures show the result: spinning 100 pounds of cotton took an Indian hand spinner about 50,000 hours, Crompton’s mule about 2,000, and the automatic self-acting mule of the 1820s only 135. No hand spinner anywhere could compete with machines that cut the labour by more than ninety-nine per cent.
The short answer
- Indian cloth set the standard. Indian calicoes, printed cotton cloths, showed Europeans what cotton could be: light, washable, cheap and dyed in colours that did not run. When Parliament banned printed calicoes in 1700 and their wearing in 1721 to protect English wool, it left a large home market that British producers could fill only if they matched Indian quality at Indian prices. Import substitution, meaning the effort to make at home what had been bought abroad, gave inventors a clear target and a protected space in which to reach it.
- Machines that suited the fibre. Spinning cotton is a repetitive task of drawing out and twisting fibres, the kind of motion that rollers, gears and the spinning rods called spindles could copy. Each machine solved a specific bottleneck: the spinning jenny multiplied spindles, the water frame strengthened the thread, the mule refined it, and carding engines prepared the raw fibre. Because cotton was imported, its supply could grow without competing for English farmland, so output could rise as fast as the machines allowed.
- Water power and modest capital. The first mills needed a fast stream, a building and a few thousand pounds, sums that a successful wigmaker, merchant or hosier, a dealer in stockings, could raise through partners and local banks. Richard Arkwright, the former wigmaker who patented the water-powered spinning frame, went into business with the Derby hosier Jedediah Strutt, and Samuel Greg, who founded the mill at Styal, drew on his family’s merchant and plantation wealth. The valleys of the Pennine hills in Derbyshire and Lancashire offered fast water within reach of markets and ports, which is why the first factories stand in steep, remote valleys far from the towns.
- Slave-grown cotton without limit. Cotton had to come from somewhere, and after 1793 it came above all from the American South. The inventor Eli Whitney’s cotton gin separated the seed from the short-fibred cotton that grew inland, so planters pushed slavery onto new land in Georgia, Alabama and Mississippi. The supply of raw cotton thus expanded as fast as Lancashire’s demand, kept cheap by the unpaid labour of enslaved people, whose numbers in the United States nearly tripled between 1790 and 1830.
THE TURNING POINT
Cromford Mill, 1771. The entrepreneur Richard Arkwright’s mill at Cromford, on the River Derwent, is the hinge because it was the first place where all the elements of the factory system came together: powered machines, a large workforce tending them in shifts, a manager’s rules, and housing built to keep the workers close. Earlier silk mills and workshops had some of these features, but Cromford’s model could be copied, licensed and financed, and within twenty years it had been copied in dozens of mills across Derbyshire, Lancashire and Scotland. From then on, British manufacturers argued only about how fast to mechanise.
What it changed
Steam moves the mills to the towns. Water power tied mills to remote valleys, and from the 1790s steam engines freed them. Manchester’s mills clustered beside canals that brought coal, and the cotton district spread across south Lancashire, where coal, labour and the port of Liverpool lay close together. Chapter 3 explains the engine that made this possible, and chapter 5 the towns it created. Steam let the industry grow wherever coal could be delivered.
Child labour becomes a public question. The pauper apprentices of Styal, destitute children sent to work for their keep, and the children who worked twelve-hour shifts in Manchester’s mills became the subject of parliamentary inquiries from 1816 onwards. The mill owner Robert Owen argued from the example of his own model mill at New Lanark, the politician Michael Sadler’s committee of 1832 gathered testimony from the workers themselves, and the Factory Act of 1833 finally enforced limits on children’s hours with paid inspectors. Chapter 5 follows that struggle in Parliament and the mills. The children’s own testimony became the evidence that changed the law.
The handloom weavers’ boom and ruin. Machine-spun yarn first multiplied the work of handloom weavers, who were well paid until about 1805, and then drew so many recruits into the trade that rates fell. When power looms, mechanised weaving machines, spread in the 1820s and 1830s, weavers’ piece rates, the pay for each length of cloth, collapsed and many families fell into poverty. Their anger fed the machine-breaking and protest of chapter 6. Their fate showed that a machine could destroy a skilled trade within one working life, faster than any family could retrain or move.
Lancashire depends on the plantation South. By the late 1850s about three-quarters of Lancashire’s cotton came from the slave states of the American South, a dependence that tied Britain’s largest industry to the fate of slavery. When the American Civil War cut the supply in 1861, Lancashire’s mills fell silent and the trade turned to India and Egypt, the story that chapter 11 tells. The crisis showed how dangerous it was for Britain’s largest industry to depend on a single slave-worked region.
The full answer, argued
The machines were real and their gains enormous. A self-acting mule, an automatic spinning machine, spun in 135 hours what an Indian hand spinner needed 50,000 hours to spin, and no amount of discipline could have produced that difference by itself. Yet the first factories brought machines and workers together under one roof partly for reasons of control. The rules and child apprentices of the mill owners Richard Arkwright and Samuel Greg, together with the fines and bells of Manchester’s mills, show employers solving the problem of making people work steadily, a problem the domestic system, in which spinners and weavers worked at home for merchants, could not solve. The historians Sidney Pollard and E. P. Thompson emphasise this side, the economist Stephen Marglin pushed it furthest, and the economic historians David Landes and Robert Allen stress the technology. The most persuasive answer treats the two as inseparable, because expensive machines paid only if they ran without pause, and they ran without pause only if workers were disciplined to tend them. The wider lesson is that a new technology usually arrives together with a new way of organising people, and both have to be explained.
An interesting fact
Samuel Crompton, who in 1779 invented the spinning mule, a machine that spun fine yarn, could not afford to patent it. He released the design to manufacturers who promised him a subscription, a fund raised from their voluntary contributions, and received less than £70. In 1811 he toured the cotton districts counting spindles, the thread-twisting rods, to support a claim for a public reward, and he estimated that some 4.6 million of them were now spinning on mules. In 1812 Parliament granted him £5,000, a fraction of the fortune the mill pioneer Richard Arkwright made from his water-powered spinning frame, and Crompton died in Bolton in 1827 in modest circumstances. His mule became the standard spinning machine of the industry for a century, while the fortunes it made went to others.
This is the study layer of Cotton and the factory system, chapter 2 of The Industrial Revolution, 1750–1914; the full index of the atlas is here.
Related questions
THE FREE PRINTABLE STUDY GUIDE
Join the Dispatch — a short welcome series, then a letter when a new atlas opens — and the printable study guide for The Industrial Revolution is yours now, free.
NO TRACKING · YOUR ADDRESS IS USED FOR THE DISPATCH AND NOTHING ELSE · UNSUBSCRIBE ANYTIME